The Engineering Case for VFD Projects
Variable Frequency Drives create savings by matching motor speed to process demand instead of forcing motors to run at full speed all the time. In plants with large pump and fan loads, this changes the energy equation dramatically because the process no longer wastes power through throttling, damper control, bypass loops, or repeated mechanical starting.
The best VFD projects begin with measurement. Engineers should understand the operating profile, motor load, process variability, and utility tariff structure before specifying hardware. That context reveals whether the value comes mainly from electrical savings, improved control stability, reduced maintenance, or lower demand charges.
When the project is designed carefully, VFD installation becomes more than a motor control upgrade. It becomes part of a wider process optimization strategy that can be measured, reported, and expanded to other utility systems across the plant.
Affinity Laws and Load Behavior
For centrifugal loads, the affinity laws are the technical foundation of most energy-saving calculations. Flow is proportional to speed, pressure is proportional to the square of speed, and power is proportional to the cube of speed. That means a relatively small speed reduction can create a surprisingly large reduction in absorbed power.
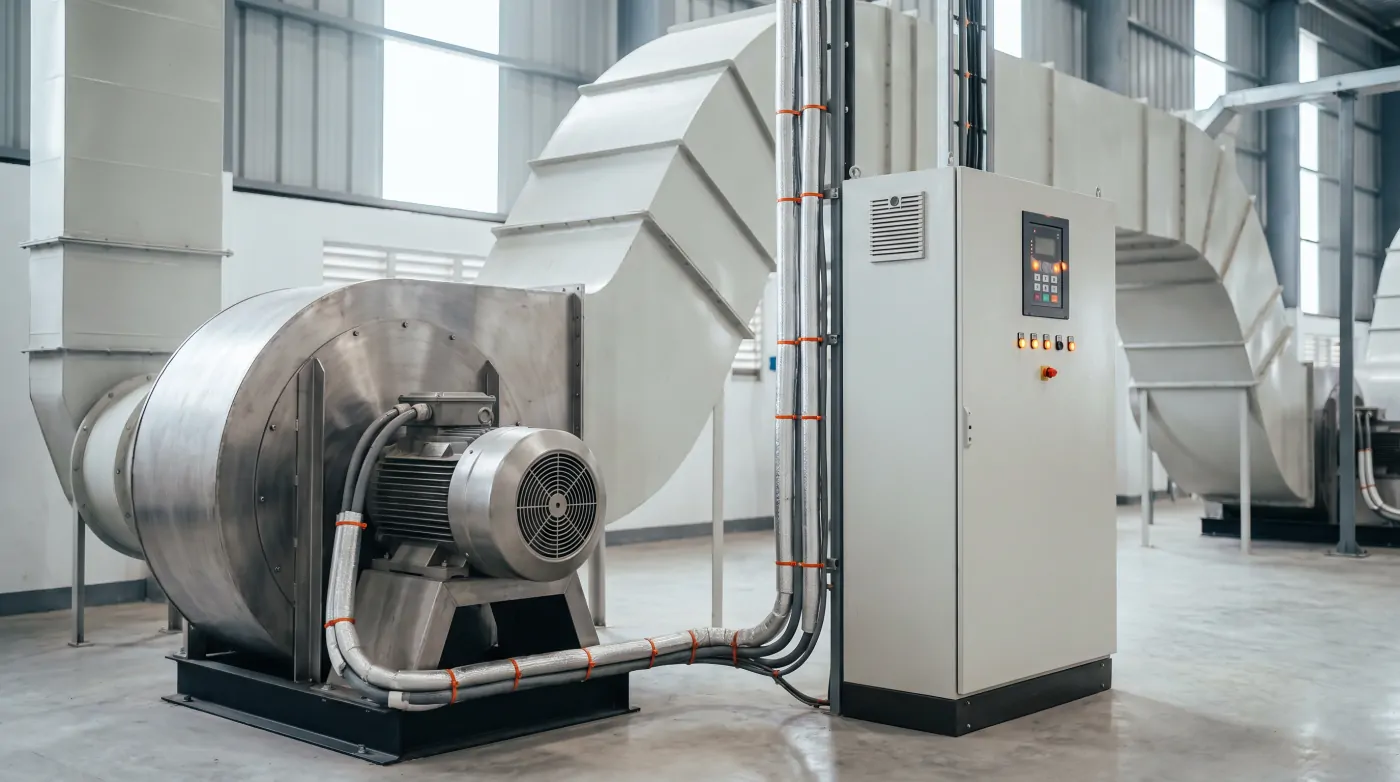
This is why pumps, cooling tower fans, exhaust blowers, and circulation systems are often excellent VFD candidates. If the process does not need full output continuously, there is no reason to keep the motor at base speed and discard the excess mechanically. The drive allows the system to operate closer to actual demand.
Not all loads behave this way, so application review matters. Positive-displacement machines, high-inertia loads, and constant-torque processes may still benefit from VFDs, but the technical justification is different and often focuses on smooth control, soft starting, and lower mechanical stress.
Sizing, Protection, and Power Quality
Drive sizing should account for motor full-load current, overload requirements, ambient conditions, enclosure cooling, cable length, and duty cycle rather than relying only on nameplate kilowatt values. If the motor serves a high-starting-torque or harsh-process application, the drive must be selected accordingly.
Power quality must also be reviewed. Harmonics, capacitor bank interaction, transformer capacity, and sensitive instrumentation on the same supply can all influence the final design. Line reactors, DC chokes, or harmonic filters may be justified depending on the number of drives and the electrical network strength.
Motor protection is equally important. Older motors may need insulation assessment, and long motor cables may require dv-dt mitigation or output filtering. Good installation practice protects both the drive and the connected motor over the long term.
Control Strategy and Process Integration
A VFD becomes most valuable when it is integrated into the machine or process logic properly. Start and stop commands, run permissives, fault handling, speed references, and local or remote control modes should all be defined clearly in PLC code. Without that structure, the drive may work electrically but still cause inconsistent machine behavior.
Setpoint control often depends on PID loops within the drive or PLC. The choice depends on the application, tuning expectations, and the wider automation architecture. For example, a booster pump set may benefit from in-drive PID with pressure feedback, while a machine line with multiple interdependent actuators may be easier to manage from the PLC.
Teams building that control layer often strengthen overall machine behavior by aligning the drive strategy with PLC Programming Basics for Industrial Automation, because drive logic is only as maintainable as the surrounding PLC structure.
Verification and Reporting
Savings claims should be verified through data. Before commissioning, engineers should capture line current, kilowatts, operating hours, pressure, flow, and production output where possible. After startup, the same measurements should be compared under equivalent process conditions to confirm the technical and financial outcome.
SCADA and historian tools make this much easier by trending drive current, speed command, output frequency, motor load, and process response over time. That evidence supports energy reporting and helps operations teams maintain the achieved performance instead of drifting back to inefficient settings.
If the drive begins spending long periods at maximum speed, that may indicate a process bottleneck, a dirty filter, a worn impeller, or incorrect setpoint tuning. In that sense, the VFD becomes both a control element and a diagnostic sensor.
Long-Term Standardization
Plants usually get the most value when VFD engineering becomes standardized. Common parameter structures, naming conventions, fault response rules, and panel design practices reduce startup time on future projects. Maintenance teams also become more effective because they are not relearning every system from scratch.
This standardization is even stronger when VFD data is visible within a plant-wide SCADA framework. Trending, alarms, and maintenance diagnostics become easier to manage across multiple lines and utilities. That is why many energy programs expand naturally into broader monitoring projects such as a SCADA System Guide for Modern Industrial Monitoring.
Over time, the technical gains from VFDs compound. Lower electrical use, reduced mechanical stress, better process stability, and better diagnostics all contribute to a stronger and more efficient operation.
Maintenance and Lifecycle Strategy
Drive reliability improves when maintenance teams treat VFDs as monitored assets instead of sealed boxes. Cooling airflow, terminal tightness, warning logs, panel temperature, and recurring overload behavior should all be reviewed periodically so the plant can act before a trip becomes a shutdown event.
Lifecycle planning also includes spare strategy and parameter backup. If the application file, communication settings, and commissioning notes are documented properly, replacement becomes much faster and less risky. That preparation is often what separates a resilient drive program from one that suffers long downtime after a failure.
When energy savings, process stability, and maintainability all improve together, the VFD project creates a broader operational return than electricity reduction alone. That is why the strongest sites standardize their drive practices across utilities, machine lines, and service routines.
Implementation Checklist and Field Validation
Every strong automation article should connect design theory with field execution. In real projects, technical success depends on documentation, site validation, commissioning discipline, and operator adoption just as much as it depends on component selection. Engineers should define the process objective clearly, confirm actual field constraints, validate instrument health, review panel and cable conditions, and document the before-and-after operating state so the final result can be measured rather than assumed.
A practical implementation checklist usually includes hardware verification, I-O confirmation, network or communication checks, parameter backup, alarm review, and operator workflow validation. It should also include a handover package that covers drawings, configuration backups, version notes, recommended spares, and maintenance checkpoints. These steps reduce lifecycle risk and make future troubleshooting far easier, especially when the system is later expanded or connected into plant-wide reporting.
Field validation should test abnormal conditions as well as normal operation. A system that behaves correctly only under ideal conditions is not ready for production. Teams should review startup behavior, stop behavior, loss-of-signal scenarios, communication faults, and realistic operator interactions. That process reveals design assumptions early and gives the plant a more resilient final outcome. When this level of discipline is applied consistently, long-form technical content becomes genuinely useful to engineering teams because it reflects how automation projects succeed in the field rather than only how they look on paper.
Optimization, Documentation, and Continuous Improvement
Technical articles also create the most value when they frame automation work as an ongoing improvement cycle rather than a one-time installation. Once a system is stable, teams should continue reviewing trend data, alarm frequency, operator interventions, maintenance records, and power or production KPIs to see whether the design is still performing as intended. Small adjustments to control logic, tuning, alarm thresholds, or operator workflow often create significant operational gains when they are guided by measured plant behavior.
Documentation must support that improvement cycle. Good documentation includes not only final settings and drawings but also the engineering intent behind critical decisions. If a minimum drive speed was selected to protect pump cooling, if an alarm delay was chosen to avoid nuisance trips during startup, or if a communication timeout was tied to process safety, those reasons should be captured. Future engineers and technicians make better decisions when they understand the design logic instead of seeing only the final configuration values.
Continuous improvement also depends on communication between departments. Operations may notice instability first, maintenance may identify the physical cause, and engineering may connect the issue to configuration or process strategy. Technical content that encourages this cross-functional review tends to produce better plant outcomes because it reflects how modern industrial systems are actually sustained over time. In that sense, a strong long-form article should help teams not only install automation correctly but also operate, maintain, and improve it with confidence.
Practical Handover for Google-Indexable Technical Content
For content teams, the final handover should also consider how the article will perform once published. Clear slugs, structured headings, descriptive frontmatter, internal links to related guides, and sitemap inclusion all help search engines discover and understand each page. Those details matter because technical articles create the most long-term value when they remain easy to find, easy to update, and strongly connected to the rest of the knowledge base. A consistent publishing workflow turns one useful article into a scalable library of indexable industrial content.
This publishing discipline also helps engineering organizations internally. When titles, categories, tags, and related links follow a repeatable pattern, the knowledge base becomes easier to navigate and easier to expand. Over time that consistency improves both human usability and search visibility, which is exactly what a technical content program needs if every article is expected to keep generating value after the first publication date.
Further Reading
- PLC Programming Basics for Industrial Automation
- SCADA System Guide for Modern Industrial Monitoring
Related Articles
Explore more technical guides from our automation knowledge base.